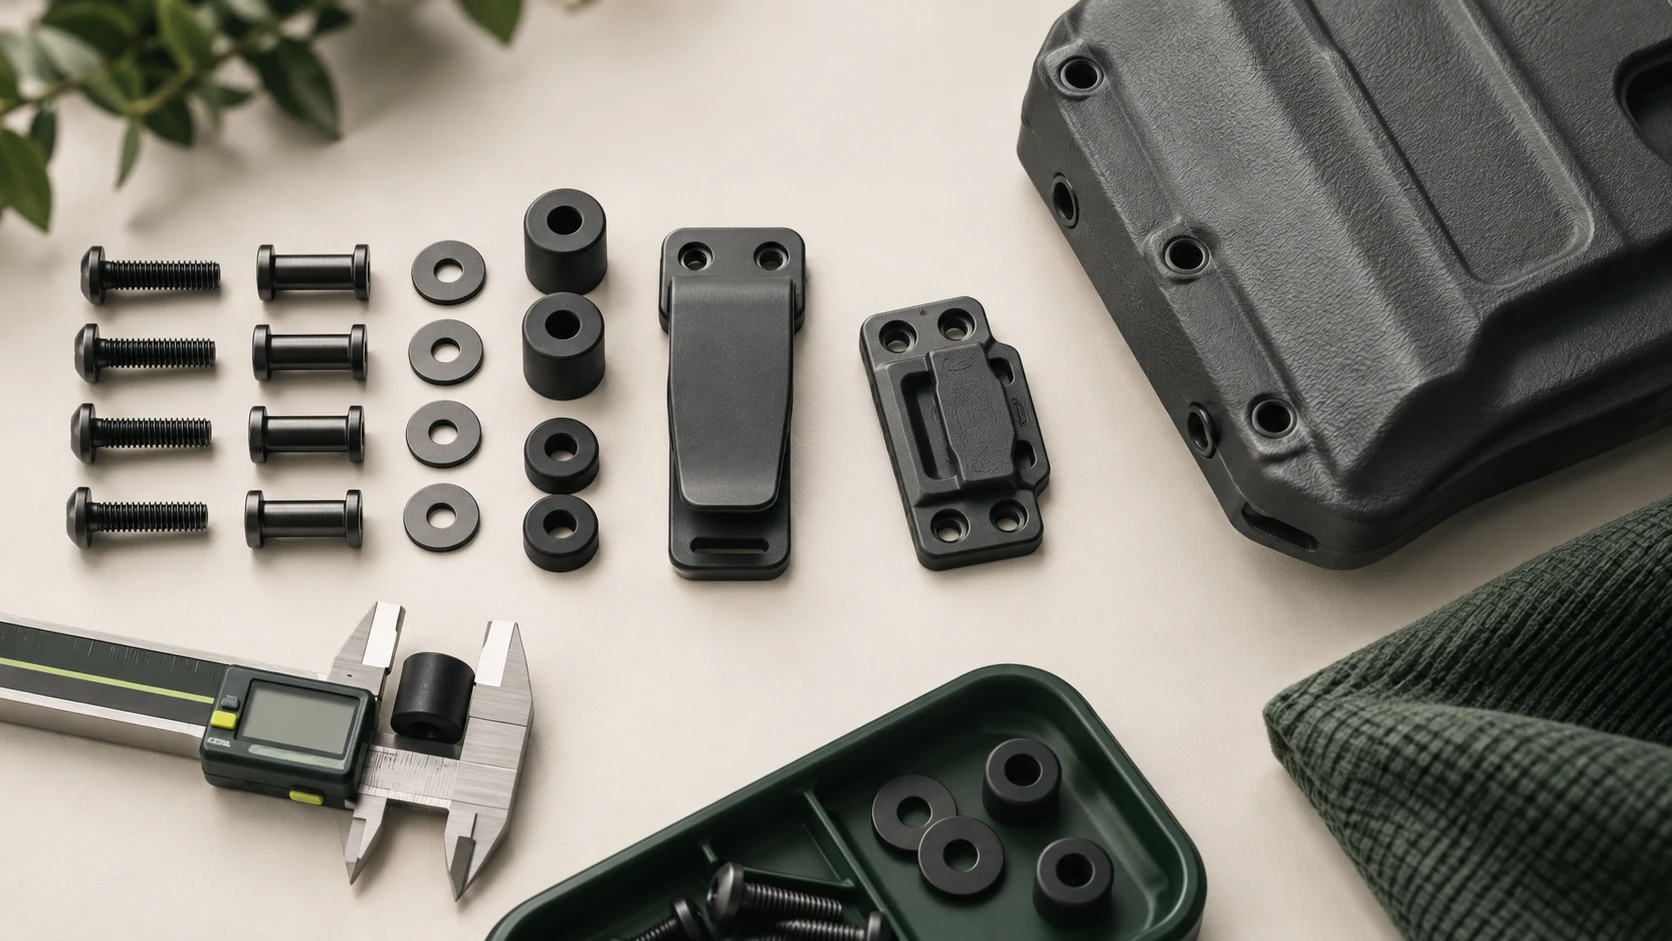
Why is the complete fastener stack important?
A screw can match the nominal thread and still be wrong for the assembly. Shell thickness, attachment thickness, washer shape, spacer compression and post length determine whether the joint clamps correctly or bottoms out, protrudes, spins or leaves insufficient engagement. Browning’s published KYDEX holster instructions, for example, identify different screw, Chicago-nut and spacer combinations for retention, belt clips and paddle configurations. This illustrates why location-specific bills of material matter.
What should the hardware specification record?
| Element | Specification fields | Assembly risk controlled |
|---|---|---|
| Machine screw | Thread, length, head style, drive, material and finish | Engagement, tool access and surface contact |
| Threaded post | Matching thread, barrel length, head and anti-rotation feature | Bottoming, protrusion and spinning |
| Washer | Inside/outside diameter, profile, material and location | Load distribution and cosmetic finish |
| Spacer | Height, diameter, hardness/material and compression condition | Retention range, stand-off and movement |
| Attachment | Approved model/interface, hole pattern and orientation | Fit, clearance and load path |
| Thread control | Approved locking method, application and service requirement | Loosening without preventing intended adjustment |
How much thread engagement is enough?
There is no universal turn count for every material and load. Bossard’s technical information on thread engagement explains that the required effective engagement depends on the material carrying the internal thread and the desired joint capacity. For an OEM carry product, define the actual mating parts, confirm that the screw does not bottom in the post, prevent unsafe protrusion, and qualify the stack with the intended load and service condition.
Retention hardware and mounting hardware do different jobs
Retention stack
May deliberately compress an elastomeric spacer so the user can adjust shell pressure within a controlled range.
Attachment stack
Secures a belt, MOLLE or modular interface and must preserve alignment, clearance and load transfer.
Fixed assembly
Uses a released clamp condition and anti-loosening method where routine adjustment is not intended.
Service kit
Must map each replacement part to the correct location and installation sequence.
Should every screw receive threadlocker?
No blanket rule is appropriate. A locking method must be compatible with the fastener finish, polymer and service plan, and it must not defeat a user-adjustable retention feature or make replacement unsafe. Specify the approved product and amount only after validation. Do not substitute an unspecified adhesive or permanent locking approach during repeat production.
OEM approval workflow
- Identify every joint and whether it is fixed, adjustable or serviceable.
- Build a location-specific exploded stack and bill of materials.
- Check clamp-up, engagement, bottoming, protrusion and tool access.
- Confirm spacer compression and usable adjustment range where applicable.
- Test the complete attachment on the named belt, MOLLE panel or host interface.
- Approve finish, corrosion expectations and cosmetic contact surfaces.
- Validate the chosen anti-loosening method and reassembly instructions.
- Lock the golden sample, torque/application method and inspection points.
Buyer release checklist
- Unique part number for each screw, post, washer and spacer
- Thread and length verified as a mating pair
- Assembly order and location shown clearly
- No bottoming, unsafe protrusion or blocked clearance
- Retention adjustment range verified where intended
- Mounting interface tested as a complete system
- Finish and corrosion expectations documented
- Locking method and service instructions approved
- Replacement kit matches the released configuration
- Incoming and final inspection points recorded
Coordinate the stack with CarryMold’s hardware and component options, belt attachment guide, MOLLE mounting options, paddle engineering guide, quality framework and first-article checklist.
Frequently asked questions
Are all 8-32 holster screws interchangeable?
No. Matching thread is only one requirement; length, head, drive, material, finish, post depth, washer and spacer stack must also suit the joint.
Why does a screw tighten without clamping the assembly?
The screw may be bottoming in the post, the post may be too long, or the stack may be missing a required washer or spacer. Inspect the complete dimensional stack.
When should hardware be reapproved?
Reapprove when thread, length, material, finish, supplier, spacer, washer, attachment, shell thickness, locking method or assembly sequence changes.
Apply the fastener stack to the complete MOLLE interface
Use the MOLLE mounting platform guide to connect posts, screws, spacers and adapters with webbing footprint, orientation, anti-rotation and installed-load checks.
Control every joint as a complete assembly.
Share the application, target quantity and launch requirements. We will outline the most practical sampling path.